
Description
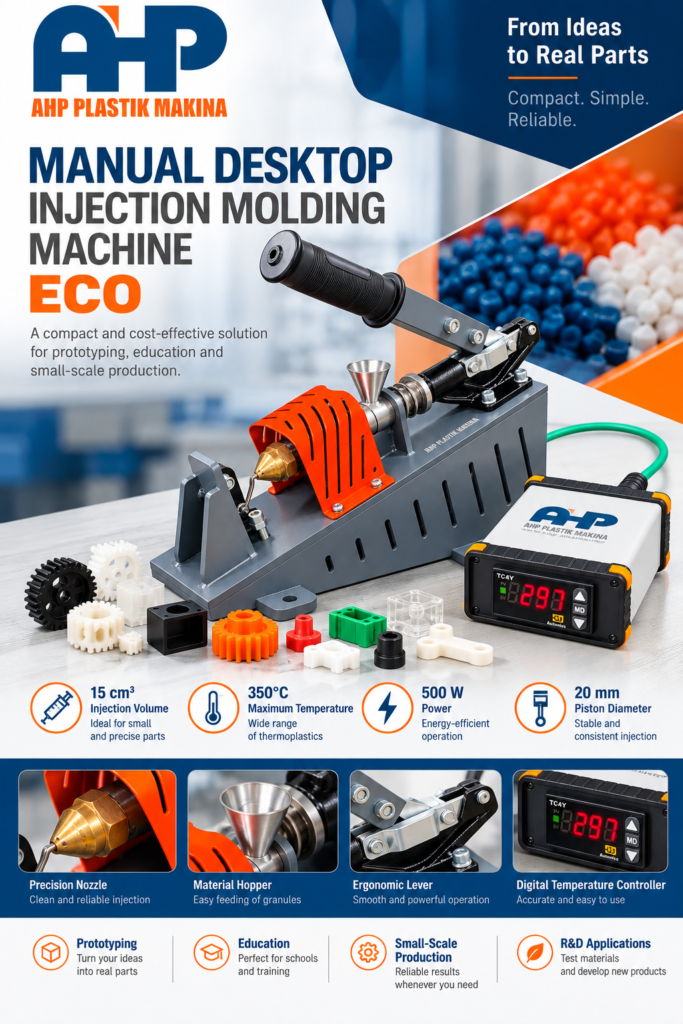
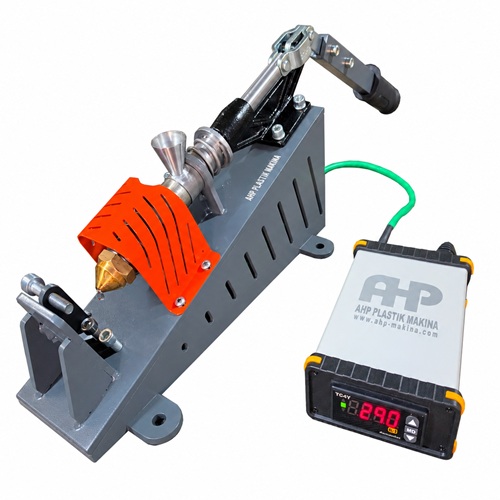
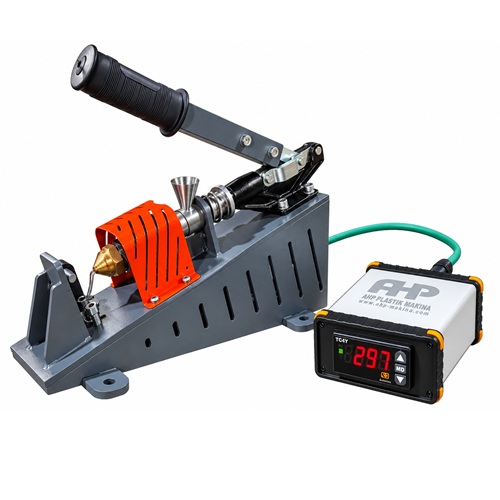
- Nominal injection volume: 15 cm3
- Operating temperature: up to 350 °C
- Power: 500W- 220V
- Easy mold change
- No need of any moving parts for charging the cylinder (compare to other brands)
- Filling the reservoir of material rapidly and easily
- Material reservoir with cooling action on the cylinder
- Robust structure guaranties no movement of parts during injection
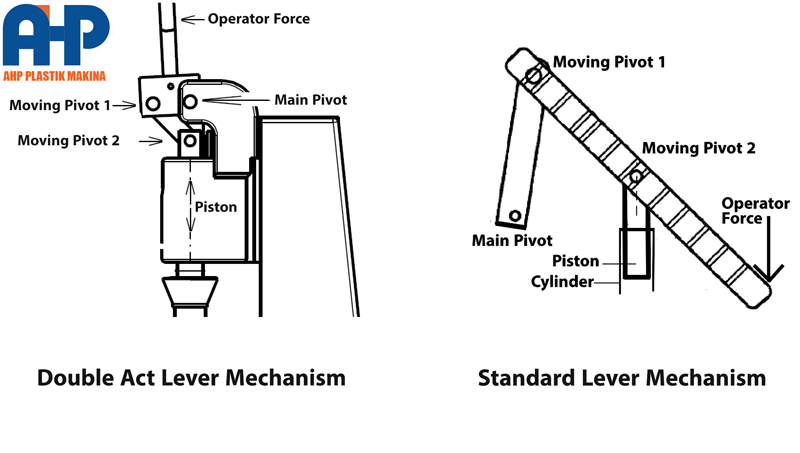
- No need to clean the piston every time because it has no touch of molten material
- Pressure application of molten material with no touch of piston head with molten material
- Doubled the force compare to the present models in the market
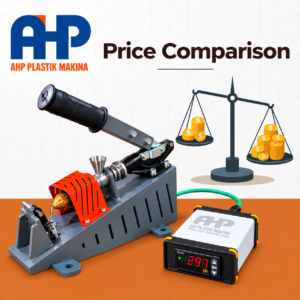
- Half price compare to the other brands in the market
- Piston diameter: 20mm (Thanks to special design for lever make it possible of doubling the force compare to other brands in the market and make it possible for higher volume of material to be injected)
- PID temperature controller
- Controller box separate from the body to be away from heat and molten material
- No grip is needed for placement of mold under injection
- Can be supplied with aluminum molds as per customer request
- Proper choice even for low flow-high MFI value materials for industrial purposes
- Easy clean of cylinder because it is easy to detach from the machine body
- Highly polished cylinder
- Double act lever mechanism increase the molding force two times compare other brands while keeping the lever length shorter
- You can even injection mold with materials like HDPE with low MFI of about 0.2 g/10 min for laboratory samples
- Safety gloves included
- Molds can be supplied with materials of customer request such as Steel, aluminum, copper …
- Compatible with different polymer materials like PEDH, LDPE, PP, PLA, PS, PA, TPU, POM, ABS, PMMA
| Parameter | New Version of AHP | Others |
| Injection volume | We used a 15mm Cylinder and a bigger shot size, even with reduced travel | Using a cylinder of 16mm because of not being able to inject material in a cylinder with a bigger diameter, due to limitations on force application, and a weak body (Most of them are less than 12 cc) |
| Force Value (Kg) | 670 KG | Most of them are less than 500 Kg (This force is applicable with hanging a man of 100 Kg with the lever of the machine with a ratio of 5/1). In most of the machines, this lever ratio is even around 4. Meaning maximum force is up to 400 Kg. |
| Reservoir | It has a reservoir with cooling, no moving parts, no melting of material inside the reservoir, and no moving parts of the head to fill the cylinder | Most of them have no reservoir, or a reservoir in contact with the hot section causes melting of some of the material inside the reservoir, with no cooling, or a reservoir that needs moving parts of the head (translation or rotation of the head) to be able to fill the cylinder |
| Force application | Double-act lever, doubled the force value | Standard lever |
| Mold grip | No mold grip, thanks to the wedge application | Manual mold grip, opens on injection of low MFI materials or higher force application |
| Injection speed | Lower travel of the piston, bigger diameter guarantees a higher injection speed and complete filling of the mold, even with low-MFI materials | Lower diameter, higher travel of the piston, on different models of lever and wheel mechanisms, causes lower injection speed. Lower speed causes solidification of the material, especially on low-flow materials inside the mold, before complete filling. |
| Shot size | 15 cc | Mostly 10-12 cc |
| Charging the cylinder | Thanks to the cooled hopper | Moving parts of the head are available, a waste of time, and charging is needed for every shot of injection. |
| Lever mechanism | Double-act mechanism, higher force, lower travel, lower lever length | Standard lever, long lever requires much effort for the operator |
| StructureR | Robust structure | Aluminum table and body, iron sheet metal working |
| Injection speed | Higher speed because of the bigger diameter, of less travel in the injection section | Less speed, because of higher travel of the piston, direct contact of the piston and molten material. Material slipping around the piston head and shaft causes friction between the molten material and the piston shaft, less force being applied to the molten material. Prolonged lever length causes lower speed. |
| MFI range suitable for injection | All ranges of material MFI is possible specially for industrial purposes and industrial laboratory applications. | Absolutely impossible to inject very low MFI materials for industrial purposes. Most of them are only suitable for general-purpose uses in home applications. |
Melt Material Has No Contact With Piston and Rod
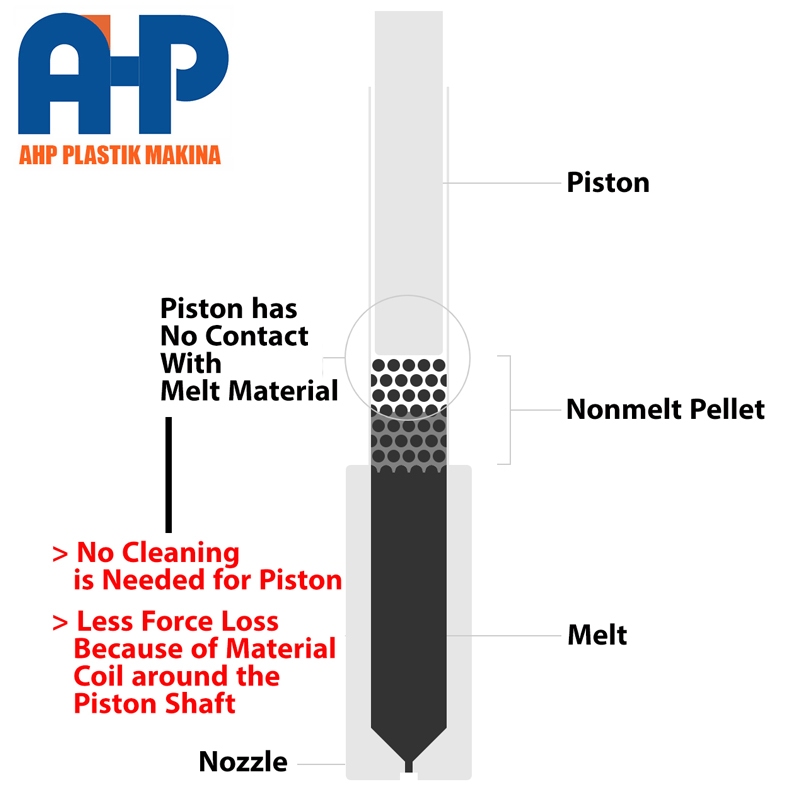
Double Act Lever Mechanism
Positioning of the pivots are in such a way that it increases force as it moves forward, compare to standard lever that you have reduction of force as operator hand moves forward. It guaranties the complete filling of the mold specially with low MFI materials for industrial laboratory purposes of tensile, Izod, Charpy, …
At the end of the injection cycles it makes it easy to keep the compaction force for cooling of sample with no formation of air bubbles on samples that is very critical specially for laboratory samples. This is because of special linkage design.
Cooled Hopper and Material Reservoir
No need to any moving hopper like translation or rotation of head parts to be able to fill the cylinder. Thanks to fixed cooling hopper and reservoir. Having moving parts at the head while taking the piston out of the cylinder for charging it, brings melt material come into contact with the head parts and making them dirty and it is difficult to clean.
Electric Panel
Separate from main body to be away from molten material and heat
Nozzle Valve
Valve for nozzle makes it possible to compact material during melting. Compaction make the melt material free of air. This is crucial parameter specially for laboratory applications for making different test samples.
Price Comparison
Cast structure makes it possible to reduce the price of finished product compare to other brands. We reduced machined parts, time of machining and assembly time. That why you will pay less money for having manual injection molding machine.